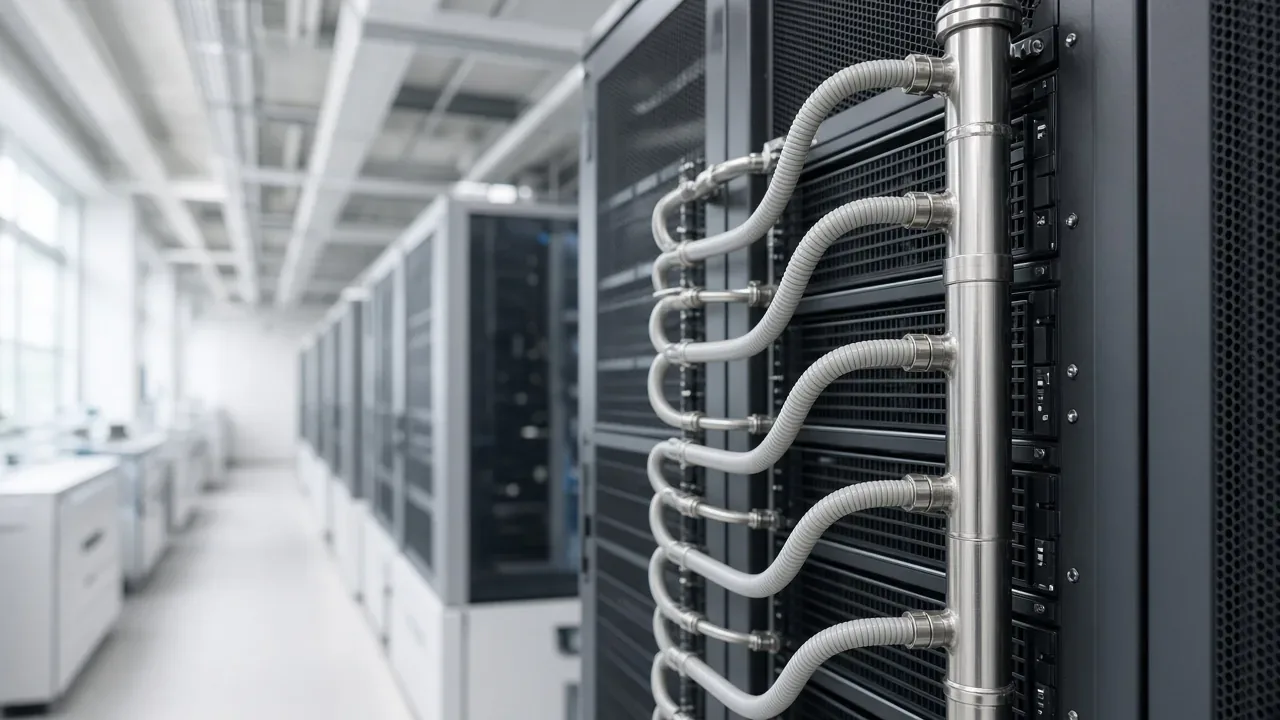
A liquid cooling manifold is the stainless steel spine that runs up the back or side of a rack and feeds coolant to every server in it. The manifold itself is simple. The valves bolted to it decide whether a technician can pull one server at 3 a.m. without draining the rack, and whether a small weep becomes a shutdown.
This guide covers the valve positions on a rack manifold and its upstream piping, what each position actually calls for, and where a stainless ball valve belongs. It is written for the people who specify these parts: manifold builders, CDU makers, integrators and the engineers who sign off the secondary loop.
What a liquid cooling manifold does
A rack manifold distributes coolant from the coolant distribution unit to the cold plates inside the servers, then collects the warm return and sends it back. A coolant distribution unit, usually shortened to CDU, is the pumping and heat exchange station that keeps the IT side of the loop separate from facility water. The closed loop between the CDU and the servers is called the secondary fluid network.
Manifolds come as vertical in-rack units, horizontal units that take rack space, and row manifolds that feed several racks. The format changes the bore size and the number of takeoffs, not the valve logic. Every design has to answer the same three questions: how do you isolate one branch, how do you drain it, and how do you get air out at the high point.
The loop, end to end
Three loops sit between the chiller and the chip, and the valve requirements change at each handover. Knowing which loop a part belongs to settles most specification questions before they start.
| Loop | What it carries | Valve duty |
|---|---|---|
| Facility water system | Building chilled water, open to the plant room | Large bore isolation, strainers, balancing, usually flanged or grooved |
| Secondary fluid network | Treated coolant on the IT side of the CDU heat exchanger | Rack isolation, drain, vent, filtration, pump check valves |
| Server branch | Coolant from the manifold to the cold plates | Dry-break quick disconnects, nothing else |
The CDU is the wall between the first two. Facility water can be hard, aerated and shared with equipment nobody inspects; the secondary loop is closed, treated and filtered, and the hardware in it is chosen to keep it that way. A valve that would be unremarkable in a plant room becomes a contamination question once it is on the IT side of that heat exchanger.
The valves on a rack manifold, position by position
There are five valve positions on and around a rack manifold. Only two of them are usually ball valves, and one of them is not a valve most valve makers can sell at all.
| Position | What sits there | Typical size | What the published specs show |
|---|---|---|---|
| Branch isolation on the manifold | Ball valve | Up to 1 in | nVent lists stainless ball valves on the branch takeoffs of its RackChiller rack manifold, on a 304L stainless body, with the assembly tested to 150 psi |
| Server connection | Dry-break quick disconnect | 1/8 in to 1 in hose | Vertiv, Danfoss, Parker, Stäubli and CPC all build valved couplings that shut off on both halves as they part |
| Upstream shut-off to the rack | Ball valve | 1 in and up | Vertiv ships its in-rack manifold with a drain valve only and states that the external shut-off valve is selected by the engineer of record |
| Drain point | Small ball valve or drain cock | 1/4 in | Vertiv fits a 1/4 in drain connection on the manifold |
| Vent at the high point | Air bleed valve | G1/4 thread | Vertiv specifies a G1/4 air bleeder, torqued to 8 N·m |
Two of those rows deserve a longer answer, because they are where most specification arguments happen.
Why the branch isolation valve is a ball valve
Branch isolation has one job: close fully, stay closed, and open again without sticking after months of sitting in one position. A quarter turn ball valve does that with one moving part in the flow path and a seat that is pressed shut by line pressure. There is no stem thread to seize and no disc to flutter.
The redundancy pattern is worth noting. A NVIDIA patent covering rack scale liquid cooling describes isolation valves on both the supply and the return where the secondary loop meets the rack manifold, so a single rack can be closed off and worked on without lifting floor panels. Two valves per rack, not one.
Why the server connection is not a ball valve
Every server drop uses a dry-break quick disconnect. The coupling carries its own internal poppet valves that seal both halves the instant they separate, so a server can be pulled with the loop running and almost no spill. These are precision assemblies, often cleanroom built and helium leak tested, and the market is held by a handful of specialists.
This matters when you are sizing up the opportunity. The quick disconnects are the highest count and highest value flow components in the rack. They are also a different product category from a cast stainless ball valve, and no amount of machining capability turns one into the other. A valve maker's place in this system is the isolation, drain, strainer and check valve positions, not the coupling.
Materials: what the published specs actually say
You will read that liquid cooling is a 316 stainless only market and that copper alloys are banned outright. The published product documents do not support that.
Vertiv's in-rack manifold manual lists the wetted materials of a product it sells today: 304 stainless, EPDM, brass and nickel plated brass. nVent's rack manifold body is 304L stainless. Neither document bans copper alloys anywhere in the secondary loop. What is true is that material choice is driven by the coolant and by the customer's own standard, and that stainless has displaced brass in some positions for durability reasons. Apollo's stainless hose cap ball valve for liquid cooled data centers is the clearest example, introduced because the brass version was not holding up in that duty.
The practical reading for a specifier: stainless is the safe default for anything that has to last the life of the rack, and the grade question is settled by the coolant chemistry, not by a blanket rule. Our valve bodies are investment cast CF8 and CF8M, the cast equivalents of 304 and 316. If the coolant carries chlorides, 316 is the grade to ask for, because molybdenum is what resists chloride pitting. If it is a treated glycol mix in a closed loop, 304 is often enough. Send us the coolant specification and we will tell you which one we would quote.
Coolant chemistry and what it does to the valve
Three fluids turn up in these loops: treated water, a propylene glycol mix in the region of 25 percent for freeze and biological protection, and dielectric fluids in immersion and some two phase designs. Each one asks a different question of the valve, and none of them is answered by the pressure rating.
Water chemistry is the one that decides the body grade. Chlorides are what pit austenitic stainless, and 316 carries molybdenum specifically to resist that. Glycol mixes are usually inhibited, and published corrosion data for inhibited propylene glycol shows acceptable rates against stainless as well as copper alloys, which is part of why brass still appears on manifold wetted material lists. Dielectric fluids raise elastomer compatibility questions rather than metal ones.
Our seats are PTFE, which is chemically inert against all three families and is the reason PTFE is the default seat material across our ball valve range. Where we will not guess is your specific fluid and additive package. Send the coolant datasheet with the enquiry and we will tell you what we would build the valve from, or tell you that we would rather not quote it.
Full port or reduced port
Full port means the ball bore matches the pipe bore, so the valve adds almost no restriction. Reduced port steps the bore down one size, which makes a shorter, lighter, cheaper valve and a measurable pressure drop.
On a coolant loop the pump has to carry that drop for the life of the system, and the branch valves sit in series with everything else. That is why the published data center ball valves are full port. Apollo's data center valve is full port, and the stainless valves other suppliers list for this duty are full port as well. Specify full port for anything in the flow path, and keep reduced port for drain and instrument takeoffs where restriction does not matter.
End connections
The manifold end of the market is not standardised the way a process plant is. Published manifolds use hose barbs, straight threads and quick disconnects on the server side, and threaded or welded connections upstream. Four options cover most of what gets asked for.
| Connection | Where it fits | Trade-off |
|---|---|---|
| Threaded, PT or NPT or PF | Branch isolation, drain points, instrument takeoffs | Serviceable, but every thread is a joint that has to be made up correctly |
| Socket weld | Fixed runs where nothing is meant to come apart | Fewest leak paths, needs a welder on site |
| Butt weld | Main runs and tight envelopes | Smoothest bore, permanent |
| Camlock | Hose assemblies and temporary connections | Fast to make and break by hand |
Camlock is worth a note. Supermicro's liquid cooling components datasheet lists a hose kit whose connector type is a ball valve with camlock ends, rated to 10 bar. That is a plain stainless ball valve doing a job in a liquid cooling build, not a specialty part.
Pressure and temperature: the ratings are not the hard part
Published secondary loop hardware runs at modest pressure. Vertiv rates its in-rack manifold at 8 bar maximum operating pressure and 0°C to 70°C. nVent tests its manifold assembly to 150 psi. Supermicro's hose kit is rated to 10 bar.
A standard stainless ball valve is far above that. Our threaded and welded ball valves are rated 1000 WOG, with a two piece high pressure build at 2000 WOG. Temperature is the number to read carefully rather than pressure: most of our ball valve range is rated −20°C to 180°C with PTFE seats, which covers coolant loop temperatures with room to spare.
The real qualification hurdles in this market are cleanliness, leak tightness and documentation, not pressure class. Ask for the mill test report with the order. We supply MTR on request and hold ISO 9001 and CE.
Seats, stems and what fails after two hundred cycles
Two valves can both be marked 1000 WOG and behave differently a year in. The rating describes the body. What fails first is almost always the seat or the stem seal, and neither is visible on a datasheet line.
A seat in a coolant loop lives an easy life thermally and a hard life mechanically. Temperatures stay well inside what PTFE handles, but the valve may be cycled every time a server is swapped, and it may sit untouched for months between those cycles. PTFE takes a set under load; the question is whether the design pre-loads the seat so it recovers. Live loaded stem packing does the same job at the stem, keeping sealing force constant as the packing relaxes. Our pneumatic three piece build uses live loaded PTFE seats with a Viton stem O-ring for that reason.
The three piece body earns its place here too. It can be rebuilt in line: undo the body bolts, replace seats and seals, put it back without cutting pipe. On a loop where draining is an event, that is the difference between a fifteen minute job and a shutdown.
Filtration and check valves: the two parts people forget
Dell's rack scale direct liquid cooling specification sets a filtration requirement on the loop, in the range of a 35 to 40 mesh screen on the facility side and 50 micron filtration on the secondary fluid network. Debris in a coolant loop ends up in cold plate microchannels, and a cold plate is not a field serviceable item.
A Y strainer is the normal way to meet that on a piping run. Ours are cast 316 with a stainless screen, rated 800 WOG, and there is a version with a blowdown valve on the cap so the screen can be flushed without opening the line.
The same Dell document places a pressure relief valve inside the CDU downstream of the pump and check valve, with a cracking pressure of 75 psi. The check valve at the pump outlet stops reverse flow when a pump in a redundant pair stops. Swing check valves suit horizontal runs, and spring loaded check valves handle vertical runs and quick closing duty.
Who specifies what
The valve on a rack manifold is rarely bought by the company that operates the data center. It is specified further up the chain, and knowing who holds the pen shortens the conversation.
| Who | What they decide | What they buy |
|---|---|---|
| Manifold and CDU builders | Body material, connection type, envelope | Valves in production quantities, often to their own drawing |
| System integrators and skid builders | The upstream shut-off, strainer and check valve that the manifold did not come with | Project quantities against a bill of materials |
| Engineer of record | Isolation philosophy, drain and vent points, filtration level | Nothing directly, but the specification follows their drawing |
| Operator | Spares and replacements | Small quantities, matched to what is already installed |
Vertiv's manual is explicit that the external shut-off valve is the engineer of record's selection. That single line explains why these valves are bought in project quantities by integrators rather than in bulk by the manifold maker.
What usually goes wrong
- Throttling with a ball valve. A ball valve is an on or off device. Partly open, it erodes the seat and gives poor control authority. Balancing belongs to a balancing valve.
- No isolation at the rack. If the only shut-off is at the CDU, a single cold plate swap takes the row down. The redundant pair at the rack takeoff is cheap insurance.
- Assuming the manifold came with everything. Vertiv states plainly that its manifold ships with a drain valve and that the external shut-off is the engineer's responsibility. That valve has to appear on someone's bill of materials.
- Buying on pressure class alone. Two valves can both say 1000 WOG and behave differently after 200 cycles. Seat material, stem sealing and cleanliness at assembly are what separate them.
- No drain or vent at the extremes. A loop that cannot be drained cannot be serviced, and trapped air at the high point starves the branch below it.
What to ask a valve supplier for
The parts are ordinary. The paperwork and the process behind them are what a buyer in this market is really evaluating. Five things are reasonable to ask for, and any manufacturer that cannot answer them is worth a second look.
- Leak test coverage. Ask whether every valve is tested or a sample from the batch. We test every valve before it ships, not a sample.
- Material traceability. A mill test report for the body material, available on request and called out at order time.
- Dimensional inspection. A report on request, which matters when the valve has to fit an envelope someone else designed.
- Where the casting comes from. Ask whether the supplier pours its own bodies or buys them. We cast in our own foundry, then machine and assemble on our own floor.
- Quality system. ISO 9001 and CE marking. If a certificate is not named, assume it is not held.
None of that is exotic for a valve maker. It is unusual to be asked for all five at once, which is what tells you the customer is building something that cannot be taken offline easily.
What we supply for this duty
We are a valve manufacturer in Longjing, Taichung, Taiwan. We have cast, machined and assembled here since 1995, with our own foundry and assembly floor, and we build both our own line and private label work for brands who put their name on what we make. We do not build quick disconnects, and we will say so before you ask.
| Position on the loop | Product | Body | Rating |
|---|---|---|---|
| Branch and rack isolation | Two piece ball valve | CF8 or CF8M | 1000 WOG, −20°C to 180°C |
| Isolation that has to be rebuilt in place | Three piece ball valve | 316 stainless | 1000 WOG, −20°C to 180°C |
| Welded runs | Socket weld ball valve | CF8 or CF8M | 1000 WOG, −20°C to 180°C |
| Hose assemblies | Camlock ball valve | 304 or 316 | 1000 WOG, −20°C to 180°C |
| Higher pressure builds | 2000 WOG ball valve | CF8 or CF8M | 2000 WOG, −20°C to 180°C |
| Loop filtration | Y strainer and the version with a blowdown valve | Cast 316 | 800 WOG, −20°C to 180°C |
| Pump outlet | Swing check valve or spring check valve | Cast 316 or CF8 | See the product page for the rating by type |
| Actuated isolation | Pneumatic three piece ball valve | 316 stainless | 1000 WOG, ISO 5211 direct mount |
Threads are PT, NPT or PF. Bodies are investment cast in our own foundry, machined and assembled on our floor, and seats are PTFE. Custom work is not limited to stainless: if your drawing calls for another material, send it over and we will quote it. For private label, laser marking, stamping and printed cartons to your artwork, see how custom and OEM valve work runs here, and for the valves further upstream read our guide to valves in the coolant distribution unit and secondary fluid network.
A specification checklist
Put these eight items on the drawing and most of the back and forth disappears.
- Body grade, stated as 304 or 316 rather than left to the supplier
- Port style, full port for anything in the flow path
- End connection and thread standard, PT, NPT or PF, or socket weld or butt weld
- Seat material and whether live loading is required
- Working pressure and temperature range for the loop, not for the valve
- Actuation, manual or pneumatic, with the mounting standard if actuated
- Documentation required at delivery: mill test report, dimensional report, leak test record
- Marking requirements, including private label if the valve carries your brand
Frequently asked questions
What valves go on a liquid cooling manifold?
A rack manifold carries a dry-break quick disconnect at every server drop, a drain valve at the low point and an air bleed valve at the high point. Branch takeoffs and the upstream connection to the rack use ball valves for isolation. nVent publishes stainless ball valves on the branches of its rack manifold, and Vertiv ships its manifold with a drain valve while leaving the external shut-off valve to the engineer of record.
Should the isolation valve be 304 or 316 stainless?
It depends on the coolant. 316 contains molybdenum, which resists chloride pitting, so it is the grade to specify where the fluid carries chlorides or where the customer standard calls for it. 304 is often enough in a treated closed loop. Published manifolds use both: nVent's body is 304L, and Vertiv lists 304 stainless along with brass among its wetted materials. There is no published rule banning copper alloys from the secondary loop.
Does a liquid cooling ball valve need to be full port?
For anything in the flow path, yes. Full port means the ball bore matches the pipe bore, so the valve adds almost no pressure drop for the pump to carry. Reduced port is fine on drain legs and instrument takeoffs, where restriction does not matter. The stainless ball valves published for data center duty are full port.
What pressure rating does a coolant loop valve need?
Less than most people expect. Vertiv rates its in-rack manifold at 8 bar, Supermicro's hose kit at 10 bar, and nVent tests its manifold assembly to 150 psi. A standard 1000 WOG stainless ball valve is well above that. Pressure class is rarely the limiting factor. Cleanliness, leak tightness across thermal cycles and material documentation are what decide whether a valve is accepted.
Can I use a ball valve to balance flow between branches?
No. A ball valve is an isolation device. Held part open it gives poor control authority and the seat wears where the ball edge sits in the flow. Use a balancing valve for flow distribution and keep the ball valve for full open and full closed duty. The two jobs sit next to each other on the same manifold and are not interchangeable.
Summary
The valve count on a liquid cooling manifold is dominated by quick disconnects, but the parts that decide serviceability are ordinary: a full port stainless ball valve on each branch, a redundant pair where the loop meets the rack, a drain at the bottom, a vent at the top, a strainer to protect the cold plates and a check valve at the pump. None of that is exotic. It is stainless valve work with tighter expectations on cleanliness and documentation than a plant room job.
If you are building manifolds, CDUs or the piping around them and want the isolation, drain, strainer and check valve positions quoted from one factory, send the drawing or the specification and we will price it.